In the rapidly evolving landscape of sustainability and carbon reduction, staying ahead of the curve is crucial. CANUSA EPC has curated a list of 2026 carbon-related events, conferences, and tradeshows across Canada & the USA.
Each event has been selected for its networking opportunities, panels of leading experts, and discovering cutting-edge solutions. Whether you’re a seasoned professional or just beginning your journey in the field of carbon reduction, this e-book will help you determine which event(s) you may want to attend this year. Download now and let the team at CANUSA EPC know which ones you’re attending!
Download the presentation from CANUSA EPC’s 2025 Carbon Capture and Injection Update – Market Developments. The conference incorporated new regulations, supply chain uses for CO2, and technology development for new separation processes.
Our presentation provided insights to the follow CO2 injection trend:
Concerned about water saturated CO2 causing reliability and integrity issues? Trying to determine the right dehydration technology for your CO2 injection project? Download the presentation CANUSA EPC’s Tevin Champagne delivered at the GPA Midstream 2025 Technical Conference.
Content includes:
Understanding dehydration
Carbon capture process
Traditional dehydration approaches – TEG, chillers, DEXPro & others
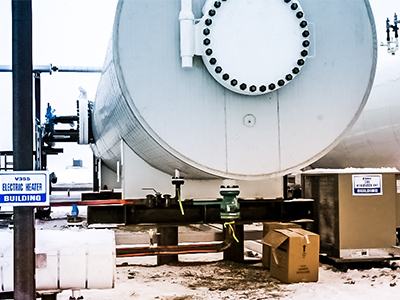
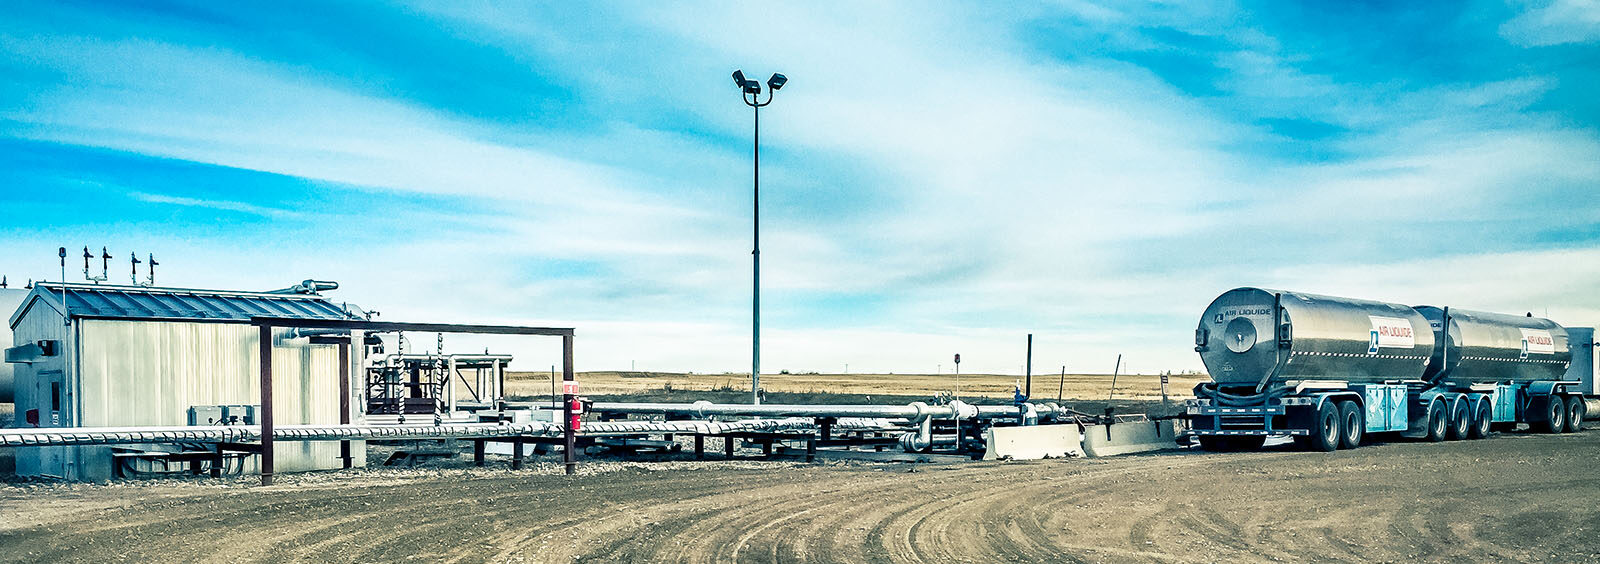
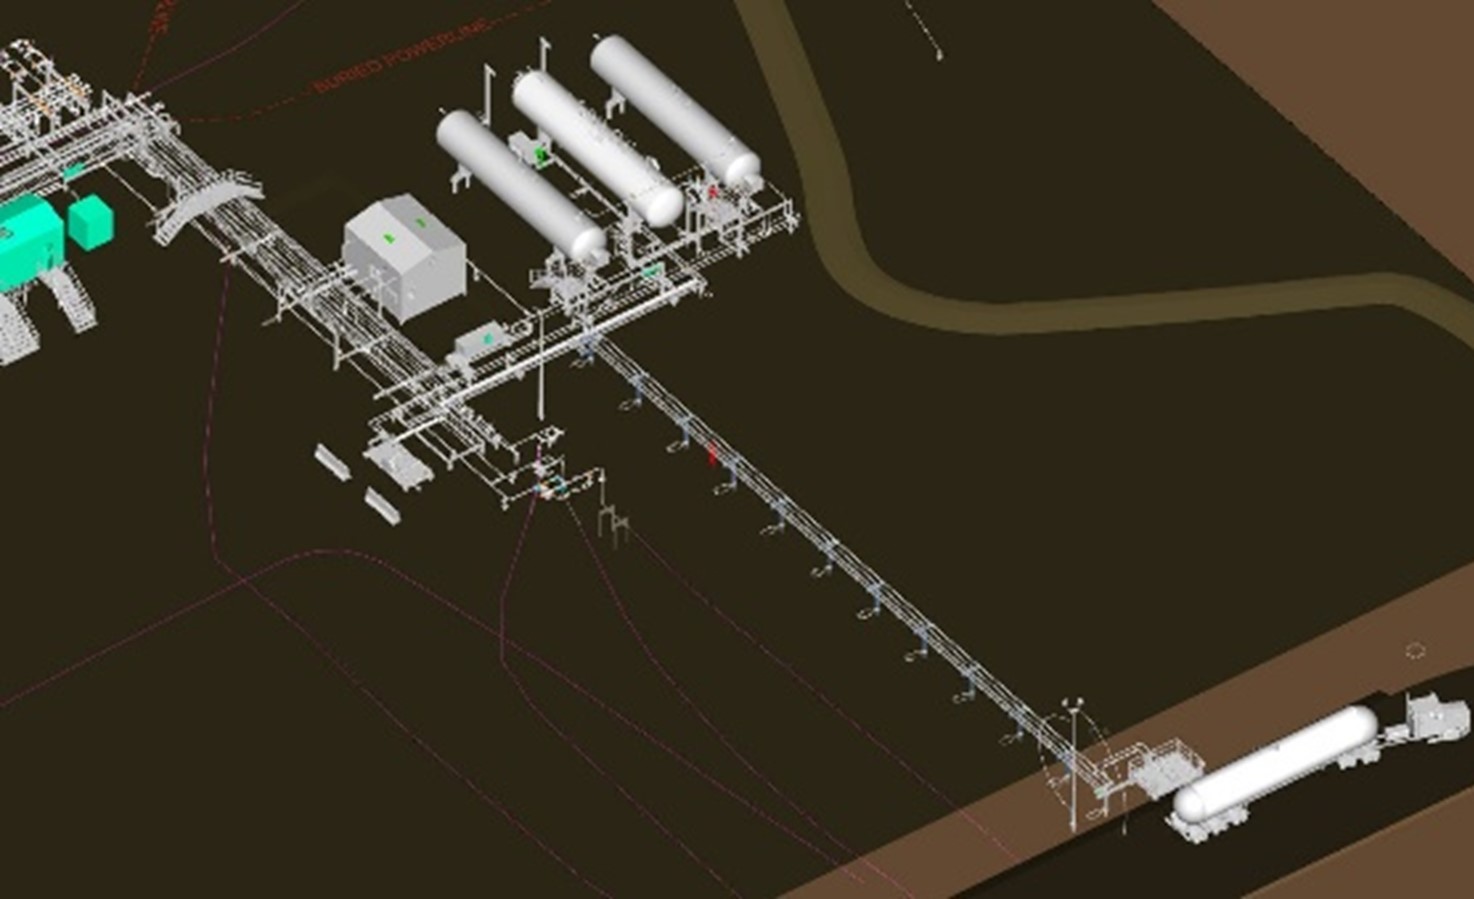
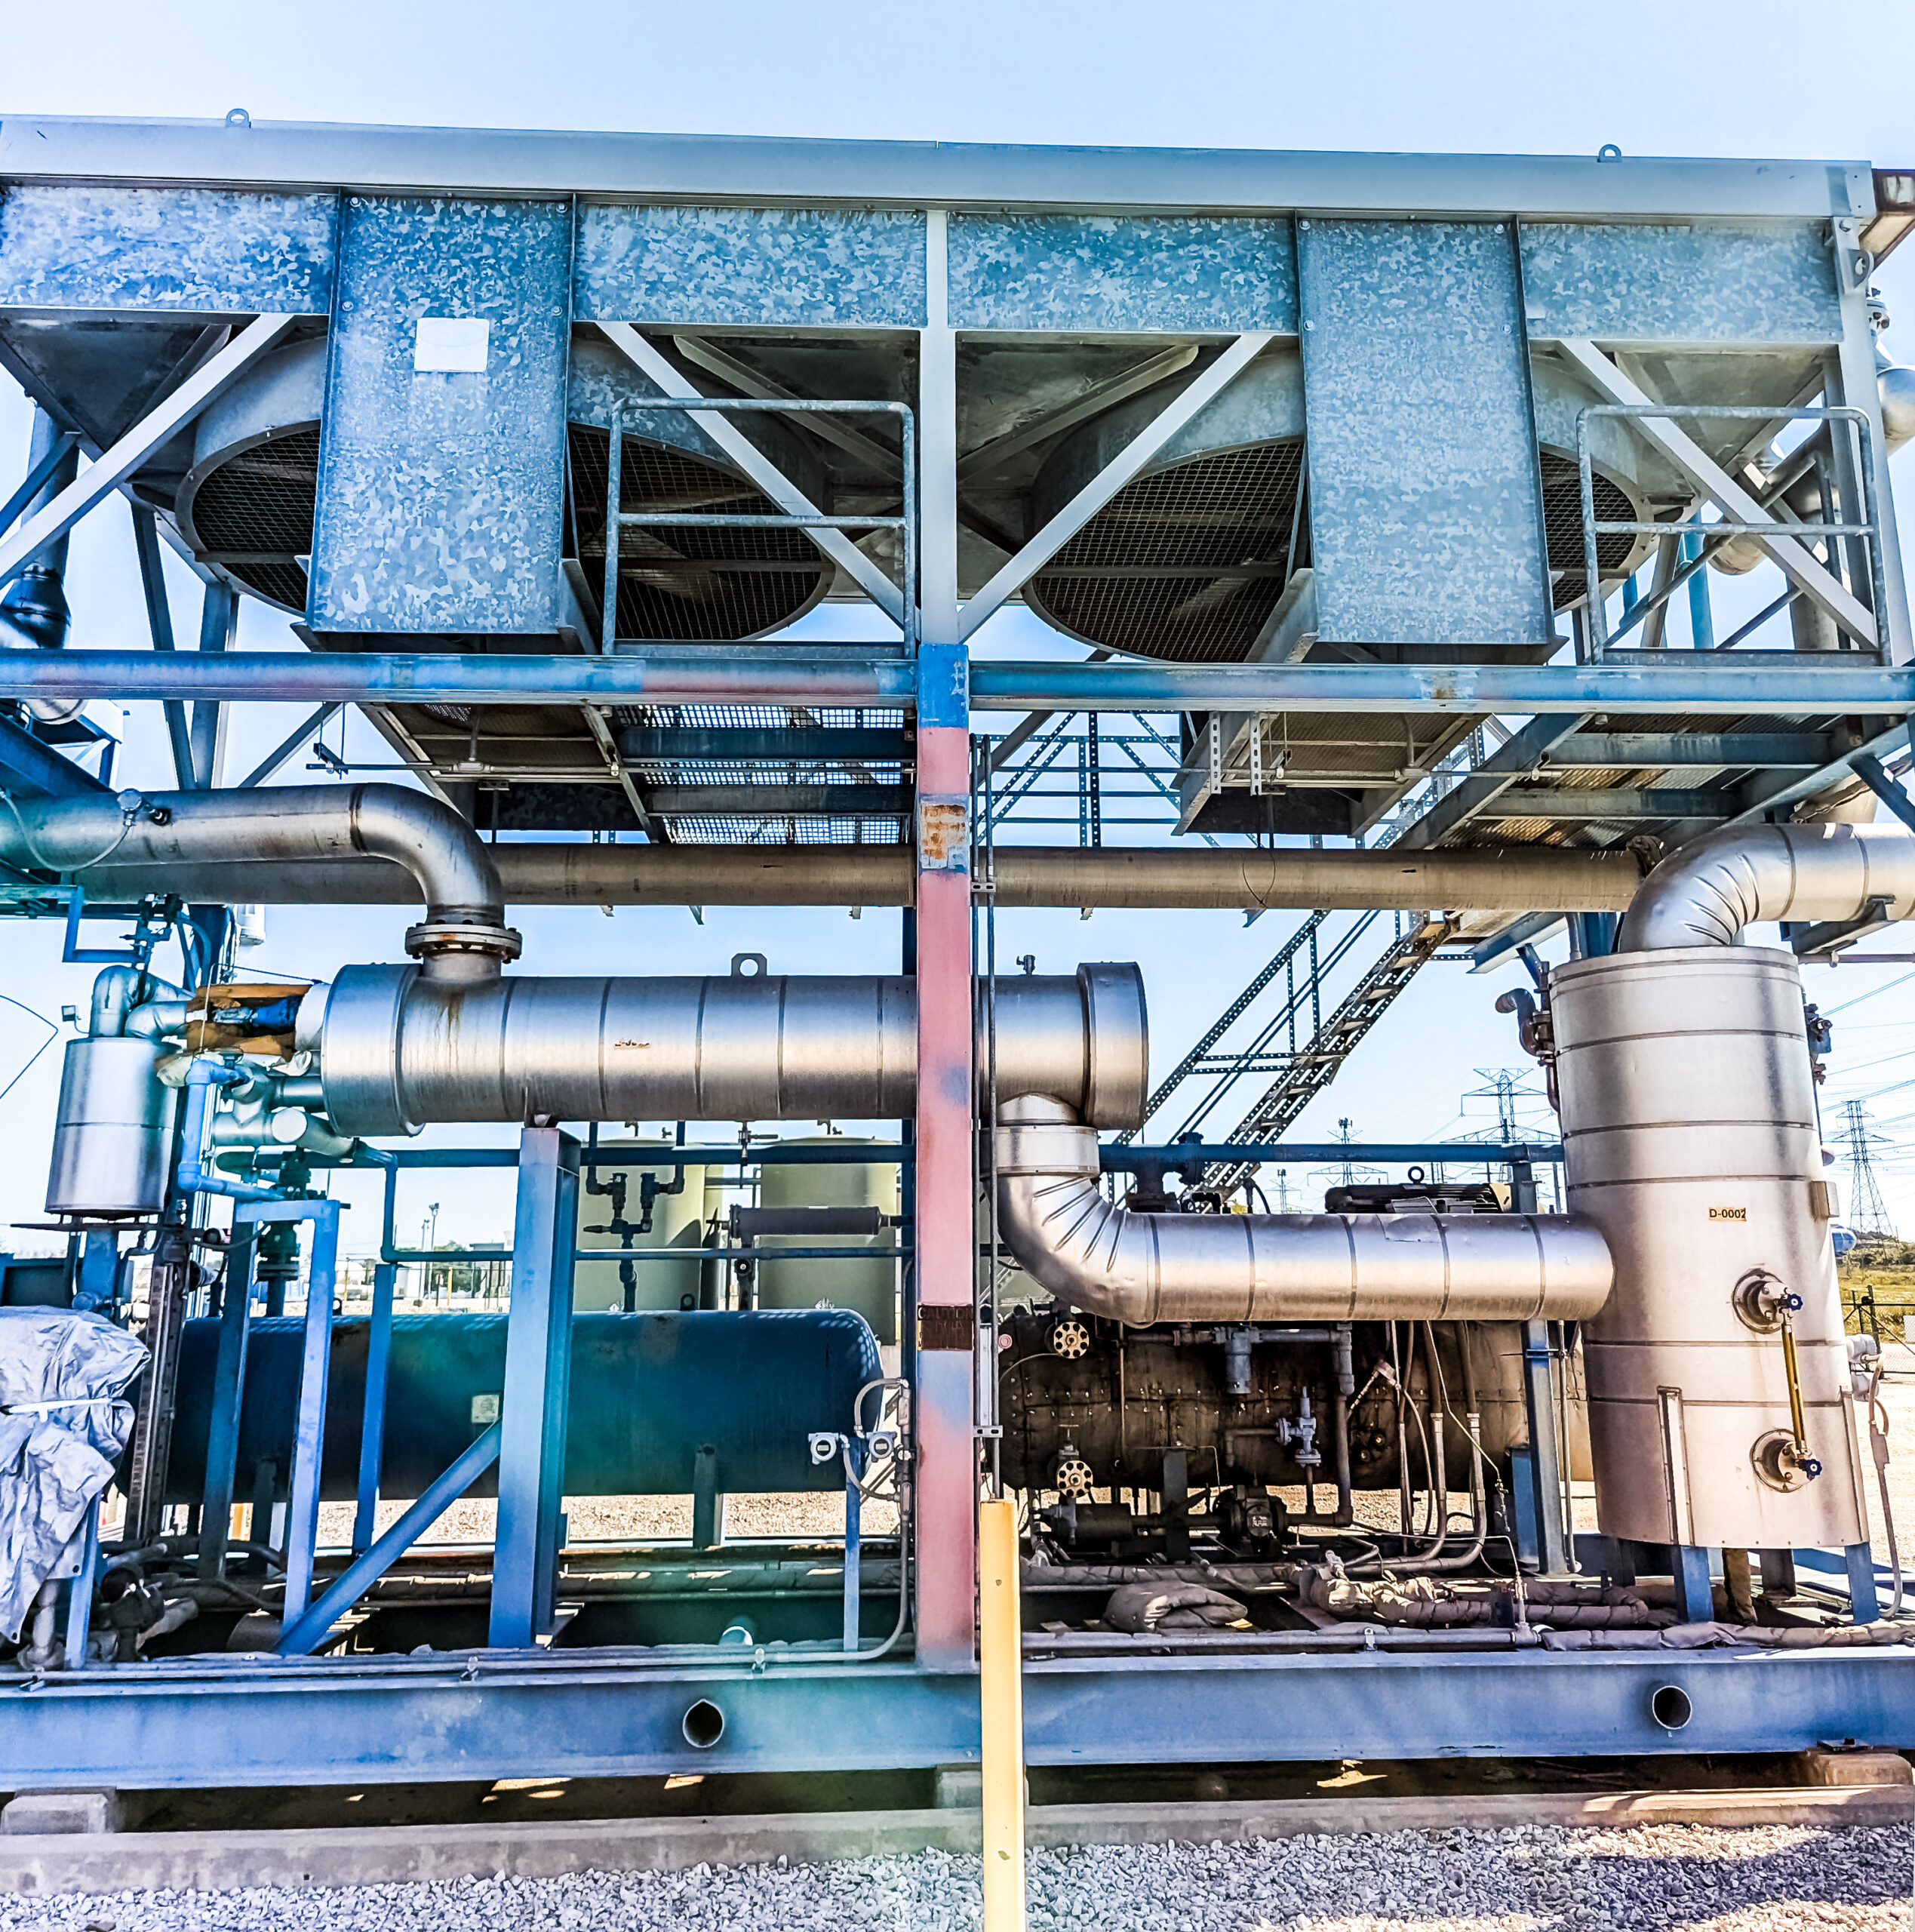
The client specialized in the development and commercialization of proprietary technologies relating to CO2 Capture & Storage (CCS) and desired to build a modular CO2 Capture System for research and industrial purposes. It was requested to provide engineering services to complete the CO2 Liquefaction design of a CO2 Capture Plant at capacities of 30 MTPD and 100 MPTD. The CO2 Capture Plant was tied into the exhaust stack of a Once Through Steam Generator (OTSG) in an oil production facility.
The Solution
Engineering:
Balance of Plant design with available and proven technologies
Separation & compression
Dehydration & purification
Refrigeration
Storage & loading
Power package & utilities
Stainless & carbon steel materials
Modularized equipment
Operations:
Seamless integration of CO2 liquefaction and CO2 capture plant
Onsite storage of 300 MTPD of liquified CO2
Dedicated liquid CO2 loading station for truck-out via third-party
The Capability
Processing of 99% CO2 and 1 % H2O with impurities
Production of ISBT Standards for beverage-grade CO2
TIC of $5MM for 30 MTPD and TIC of $8MM for 100 MTPD
Our client was facing several challenges related to the selection of dehydration technology downstream of an existing Amine Plant. The existing setup could not meet the stringent water content requirements, which was critical for the longevity of their infrastructure and the efficiency of the CO2 injection process. Their goal was to reduce the water content in their gas stream to 25 LB/MMSCF. Excess water in the system posed significant risks, including potential corrosion, hydrate formation, and inefficiencies in the CO2 injection, which could lead to operational disruptions and increased maintenance costs; so, technology selection was vital.
The Solution
CANUSA EPC conducted a comprehensive dehy technology study involving a detailed analysis of the specific operational needs of the client’s CO2 injection process, as well as the unique gas composition.
Several dehy technologies were evaluated, assessing each option based on key factors like cost, operability, risks and scalability. Technologies included: glycol dehydration, desiccant systems, and membrane technologies.
Cost Analysis:
Detailed breakdown of the CapEx and OpEx associated with each technology – provided clarity to the upfront costs but also the long-term expenses and maintenance requirements.
Risk Assessment:
Safety, reliability, and potential disruptions to the CO2 injection process. Water content control is critical in preventing hydrates and corrosion, so the risks of failing to meet the target of 25 LB/MMSCF were a major consideration.
Operability:
Focused on minimizing the need for extensive retraining or complicated maintenance procedures. We prioritized technologies that would be easy to integrate with their existing systems and infrastructure.
Future Scalability
Assessing the ability to scale was crucial – the client wanted to avoid future bottlenecks/overhauls with any future operational expansion.
The Results
Summarized detailed findings and technology options – one in particular would reliably achieve the client’s target of 25 LB/MMSCF (majority of technologies could only achieve ~50 LB/MMSCF, double the desired goal).
Report provided clarity and transparency of technology options.
Solution offered a balance of performance, cost-effectiveness, and future expandability.
Reduced risk of operational failures and ensuring confident project execution.
Testing of new technologies for capturing CO2 requires the design of the capture facility and alignment with the marketing of the CO2. A developing proprietary process is rapid cycle Temperature Swing Adsorption (TSA) systems using advanced structured adsorbents that can produce a high-purity CO2 stream. The CO2 can be pipelined for use in Enhanced Oil Recovery (EOR) production programs or utilized by CO2 consumers. The goal of pilot facilities is to demonstrate the performance and operational requirements to deploy this new technology.
The Solution
Combustion gas streams can consist of 10% CO2, 18% H2O, 70% N2, and 2% O2 with impurities
Execute the detailed design based on the supplied Process Design Basis
Plot plan & P&ID development
Civil designs & pile foundations
Structural steel & skids
Electrical, Instrumentation & Controls
Procurement
Pipeline route maps
Locate all TSA system tie-ins
Evaluate utilities
Instrument air & fuel gas
Feed & wastewater
Power loads
Design and commission control system with data acquisition and storage
Generate Standard Operating Procedures for normal, controlled, and emergency modes of operations and shutdowns
The Capability
TSA systems can capture 30 MTPD of CO2 with recovery and purity of 90%
TIC of $18MM for installation of the TSA system
Demonstrate performance and operational results from lab to pilot scale
At one of our recent ethanol projects, we were tasked with developing a relief solution for a dense-phase CO2 system. Like most early-stage sequestration sites in the U.S., this one had no simple way to recycle or offload off-spec product during a process upset. When working with dense-phase CO2, roughly 300 psi and as cold as -15°F, you’re dealing with a unique beast. It’s cold, high-pressure, and doesn’t behave like most fluids in a natural gas processing plant.
If the transport offtake shuts in or the CO2 goes off spec, the challenge becomes: how do you relieve this safely? What makes it especially challenging is how rapidly it changes states under relief conditions. This phase change can cause various operational issues and presents a massive safety hazard. API STD 521 is considered the bible, but this was one of those times when we had to look beyond the basic code.
Problems with Relieving Dense-Phase CO2
Safe operational design of CO2 capture facilities requires relief designs for dense-phase CO2 through a PSV. Relieving the CO2 liquid will induce a pressure drop and phase change, dramatically reducing the temperature during the relief. As the liquid expands, it pulls heat from its surroundings and transforms into a solid, sublimation effect. Dry ice begins to form at around -130°F. Relief temperatures can dip even lower, closer to -180°F. At these temperatures, you’re almost guaranteed to get solids that can:
Clog or choke the relief device,
Reduce flow capacity, or
Completely block the path to relief.
A blocked relief device means the vessel is no longer protected. Leaving you with a serious safety issue. As more CO2 capture and processing facilities are constructed, the normal approaches for relieving unsafe conditions won’t work for CO2. This requires that we develop solutions that protect the equipment while leveraging best practices from the industry.
Code API STD 521 and Solid CO2 Plugging Risks
API STD 521: Guide for Pressure-relieving and Depressuring Systems is the go-to standard for pressure-relieving systems, as it acknowledges this flash freezing issue. Section 4.9.2 touches on “Liquid-Vapor Mixture and Solids Formation” and warns about the potential for flashing fluids to cause choking or blockages. It also cites wet propane as an example of a fluid that can form solids.
However, there’s an issue. API STD 521 states that “some fluids (e.g. carbon dioxide and wet propane) can form solids when they are discharged through the relieving device. No uniformly accepted method has been established for reducing the possibility of plugging”.
There’s no established method to reliably predict or mitigate plugging caused by solid CO2 formation. It tells you the hazard exists but leaves the solution up to you. This was the biggest gap we have found and had to address in the design of our CO2 capture facilities.
An Approach to Pressure Relief for CO2 Processing: “Burping” CO2 Safely
We started with a question: What’s the safest way to handle relief of pressure for dense-phase CO2 that can’t be recycled or sent down the line?
One solution we have designed in our processing facilities for CO2 is to block and hold the system and send large volumes of the dense phase liquid to the distillation column through control valves that trigger based on plant upsets. The column is capable of holding large volumes of CO2 and any amount that vaporizes while being held can naturally vent through the overhead vent.
Thermal relief valves (TRV’s) are used to protect any equipment and piping that can possibly be isolated by check valves and can’t be sent to the distillation column during a block and hold scenario. While a pipeline is shut in, and if the pipeline is exposed to a heat source, such as heat from solar radiation or even ambient conditions during hot summer months, the internal process material will also heat up, expand, and increase pressure. In this case, the CO2 is at the bubble point and can vaporize with heat exposure. If thermal expansion occurs, these TRV’s will relieve this isolated high-pressure vapor, and prevent over pressurization of the system. Once the vapor is relieved, the TRV will reseat, and not allow further relieving.
This constant relieving and reseating, or “burping” of warm, vaporized CO2 will reduce the risk of relieving dense phase CO2. This approach avoided the extreme phase change that commonly resulted in dry ice plugs.
The Trading Off to Venting CO2: Safety vs. Speed
Burping CO2 is a potentially time-consuming process. The maximum amount of dense phase CO2 possible is sent to the distillation column. However, this CO2 still has to vaporize naturally. The CO2 is condensed at bubble point temperature, so the delta temperature it has to overcome is relatively small, allowing the CO2 to vaporize in a relatively reasonable amount of time. The phase change, however, still imposes temperature issues due to the Joules-Thomson effect, and still has risk of plugging up the vent piping. Careful pressure monitoring of this vent is implemented to mitigate this risk.
The remaining CO2 to be relieved by the thermal relief valves will naturally reset once vaporized CO2 is relieved, naturally mitigating the risk of freezing and plugging. Considering the size of a plant, this can quickly take a long time to relieve an entire process. At CANUSA, we believe that this careful vapor relief vs. the prevention of piping freezing and plugging method is the safest known relief strategy for dense-phase CO2 if no recycle solution is available.
CO2, unlike the relief of natural gas, is heavier than air and will sink or collect in low-lying areas. Therefore, venting locations need to be considered for safe release to ensure that de-oxygenated zones don’t form and there is adequate dispersion. Typical solutions include a vent pipe from the CO2 relief valves to higher elevations to allow the CO2 to disperse. A slower release using the Burping method will release smaller amounts of CO2 over a longer period, reducing the risk the accumulation to unsafe concentrations. OSHA incidents for CO2 handling indicate how important dissipation considerations are for the safe operations of these facilities.
Considering Process Solutions to Reduce CO2 Venting
Reducing the scenarios of release to the atmosphere not only increases the safety of the operations, but less vented CO2 will also contribute to higher capture rates and more revenue.
To reduce the scenarios of vented CO2, recycle designs can be incorporated into the process. For some facilities, a recycling approach using a closed-loop system via a cooler and blower can reduce the need to vent altogether.
This isn’t always economical. Controlled heating of dense-phase CO2 to transition to a gas phase takes considerable energy. The CAPEX of this type of system is often cost prohibitive for the low increase in recapture rate, but it could mean a true 100% capture operation.
Engineering Safety into CO2 Capture Facilities
This project made one thing very clear: the CO2 sequestration industry is evolving quickly, but the standards aren’t updating at the same speed.
We’re seeing more clients face similar problems – like what to do when a process upset sends off-spec CO2 surging through the system? API STD 521 offers the “what,” but not the “how”. Safety is vital; so, sharing solutions for the “how” is important.
Thoughtful engineering to manage dense phase CO2 during upsets
Minimal contamination of dense phase CO2 product – less than 10 ppm O2 in product
Limited venting to the atmosphere
Our team developed a practical, field-ready solution. It’s not fast. But it satisfied all of our clients’ requirements and was the safest design.
________________________________
HAVE INSIGHT ON THIS?
If you have experienced this or want to weigh in with your insights, please join the conversation on LinkedIn. Visit this post and see what others have to say!
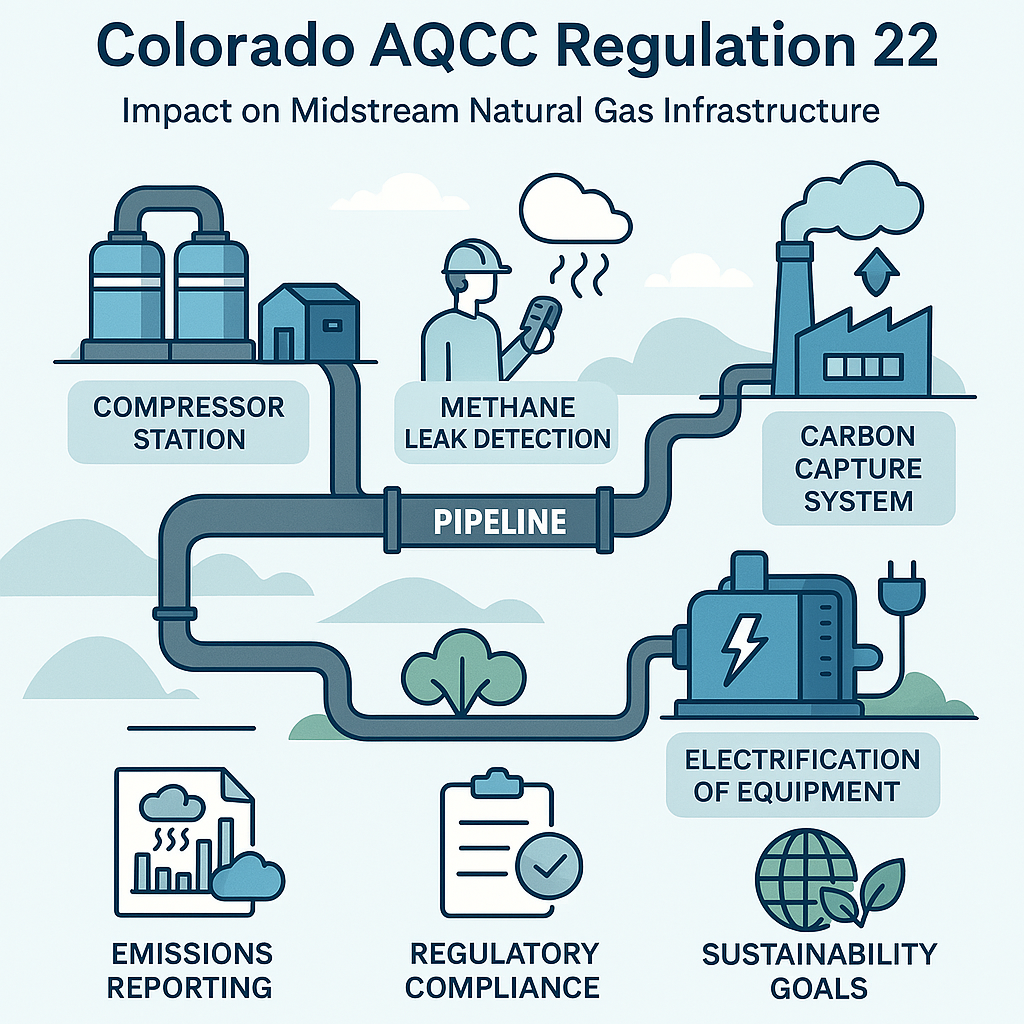
As Colorado increases its efforts to combat climate change, the regulatory landscape for industrial operators (particularly in the natural gas processing plant and gathering system sectors) is evolving rapidly. The latest development, Colorado Air Quality Control Commission (AQCC) Regulation 22, introduces stringent greenhouse gas (GHG) reporting and reduction mandates that will significantly impact how midstream infrastructure is designed, operated, and maintained.
Understanding Regulation 22
Regulation 22, formally titled Colorado Greenhouse Gas Reporting and Emission Reduction Requirements (5 CCR 1001-26), establishes a comprehensive framework for monitoring, reporting, and ultimately reducing GHG emissions across multiple sectors of the state’s economy. For midstream operators (those responsible for gathering systems, natural gas processing plants, and transportation), this regulation will require balancing the development needs of producers and the emissions caps related to GHGs.
The rule mandates that Annual GHG reporting will be required for facilities that emit over 25,000 metric tons of CO₂e per year, as well as multiple sources if they fall below the federal reporting thresholds (e.g., the 25,000 metric ton CO₂e threshold under EPA’s 40 CFR Part 98).
Emission reduction targets are aligned with Colorado’s broader climate goals: a 26% reduction by 2025, 50% by 2030, and 90% by 2050 (from 2005 levels) established under HB 19-1261.
On February 14, 2025, regulatory provisions became effective requiring every midstream company to participate in the emissions reduction program. They must achieve a collective midstream segment cap of 3,930,228 metric tons CO₂e by December 31, 2030, and maintain company-specific caps annually thereafter.
Implications for Midstream Project Development
From a project development perspective, Regulation 22, which was adopted in October 2024 and went into effect in early 2025, requires a paradigm shift. No longer can emissions be an afterthought. GHG emission reduction and methane reduction must be embedded from the earliest stages of project planning.
Here’s what midstream developers will need to consider with their emissions planning:
Carbon Footprint Assessments for New and Existing Assets
Developers must evaluate the lifecycle emissions of both current and planned infrastructure. This includes emissions from:
Compressors and natural gas processing plants
Fugitive methane leaks from gathering systems and pipelines
Combustion sources such as flares and engines
Integrating carbon modeling tools into the front-end engineering design (FEED) process is now essential to determine how overall emissions levels will be impacted for the operator. The company-specific emissions caps are calculated using each operator’s 2021 MFCE GHG emissions. October 2025 will require reporting under this program.
Technology Integration for Emission Reduction at Existing Assets
To meet reduction targets, midstream operators will consider solutions to lower the overall GHG emissions:
Electrification of engines at compressor stations and natural gas processing plants
Deployment of low-bleed or zero-bleed pneumatic devices
Advanced leak detection and repair (LDAR) programs
Carbon capture and storage (CCS) feasibility for large emitters
Operators will expect to see increased CapEx costs for compliance with marginal increases in processing capacity. Some assets may be consolidated and decommissioned before the planned end of useful life. Client will focus on reducing their methane emissions first, considered 25 times more potent than CO2 emissions. CANUSA EPC has various solutions documented for ideas, check out a novel capture application for Turbine Seal Gas Capture.
Regulatory Compliance Strategy
Operators must establish robust compliance systems that include:
Real-time emissions monitoring
Accurate data collection and reporting mechanisms
Internal audits and third-party verification
Failure to comply could result in penalties and reputational damage, especially as public scrutiny of fossil fuel infrastructure intensifies.
Civil penalties for midstream operators, under C.R.S. § 25-7-122, outline that violators may face civil penalties of up to $47,357 per day, per violation, with the amount adjusted annually for inflation. These penalties apply to a wide range of noncompliance issues, including failure to meet greenhouse gas (GHG) reduction targets, inadequate emissions reporting, and violations of leak detection and repair (LDAR) or combustion control requirements. In severe cases, the Colorado Department of Public Health and Environment (CDPHE) may also seek injunctive relief through the courts to compel compliance or halt operations.
In egregious circumstances (such as willful misconduct, repeated violations, or incidents causing serious harm), operators may also face permit suspension or revocation under C.R.S. § 34-60-121, enforced by the Energy and Carbon Management Commission. While this statute is relevant to upstream operators, it is not directly applicable to midstream GHG violations under Regulation 22 is not clearly defined. These consequences underscore the importance of strict regulatory compliance, accurate emissions tracking, and timely communication with regulators.
Looking Ahead for Natural Gas Processing Plants
Colorado’s Regulation 22 is not just a regulatory hurdle—it’s a signal of the energy transition underway. For midstream operators, aligning with these mandates is not only about compliance but also about future-proofing assets and maintaining social license to operate.
CANUSA EPC’s Role in Supporting Emissions Reductions
At CANUSA EPC, we understand the complexities of midstream development in a carbon-constrained world. Our multidisciplinary teams are equipped to:
Conduct GHG impact assessments
Design low-emission natural gas processing plants
Integrate carbon capture and methane reduction technologies
Engineer and plan electrical system upgrades
Have any questions or concerns?
Reach out to our team or start a free Class V estimate today to evaluate pathways to low-cost compliance for lower emission operations.
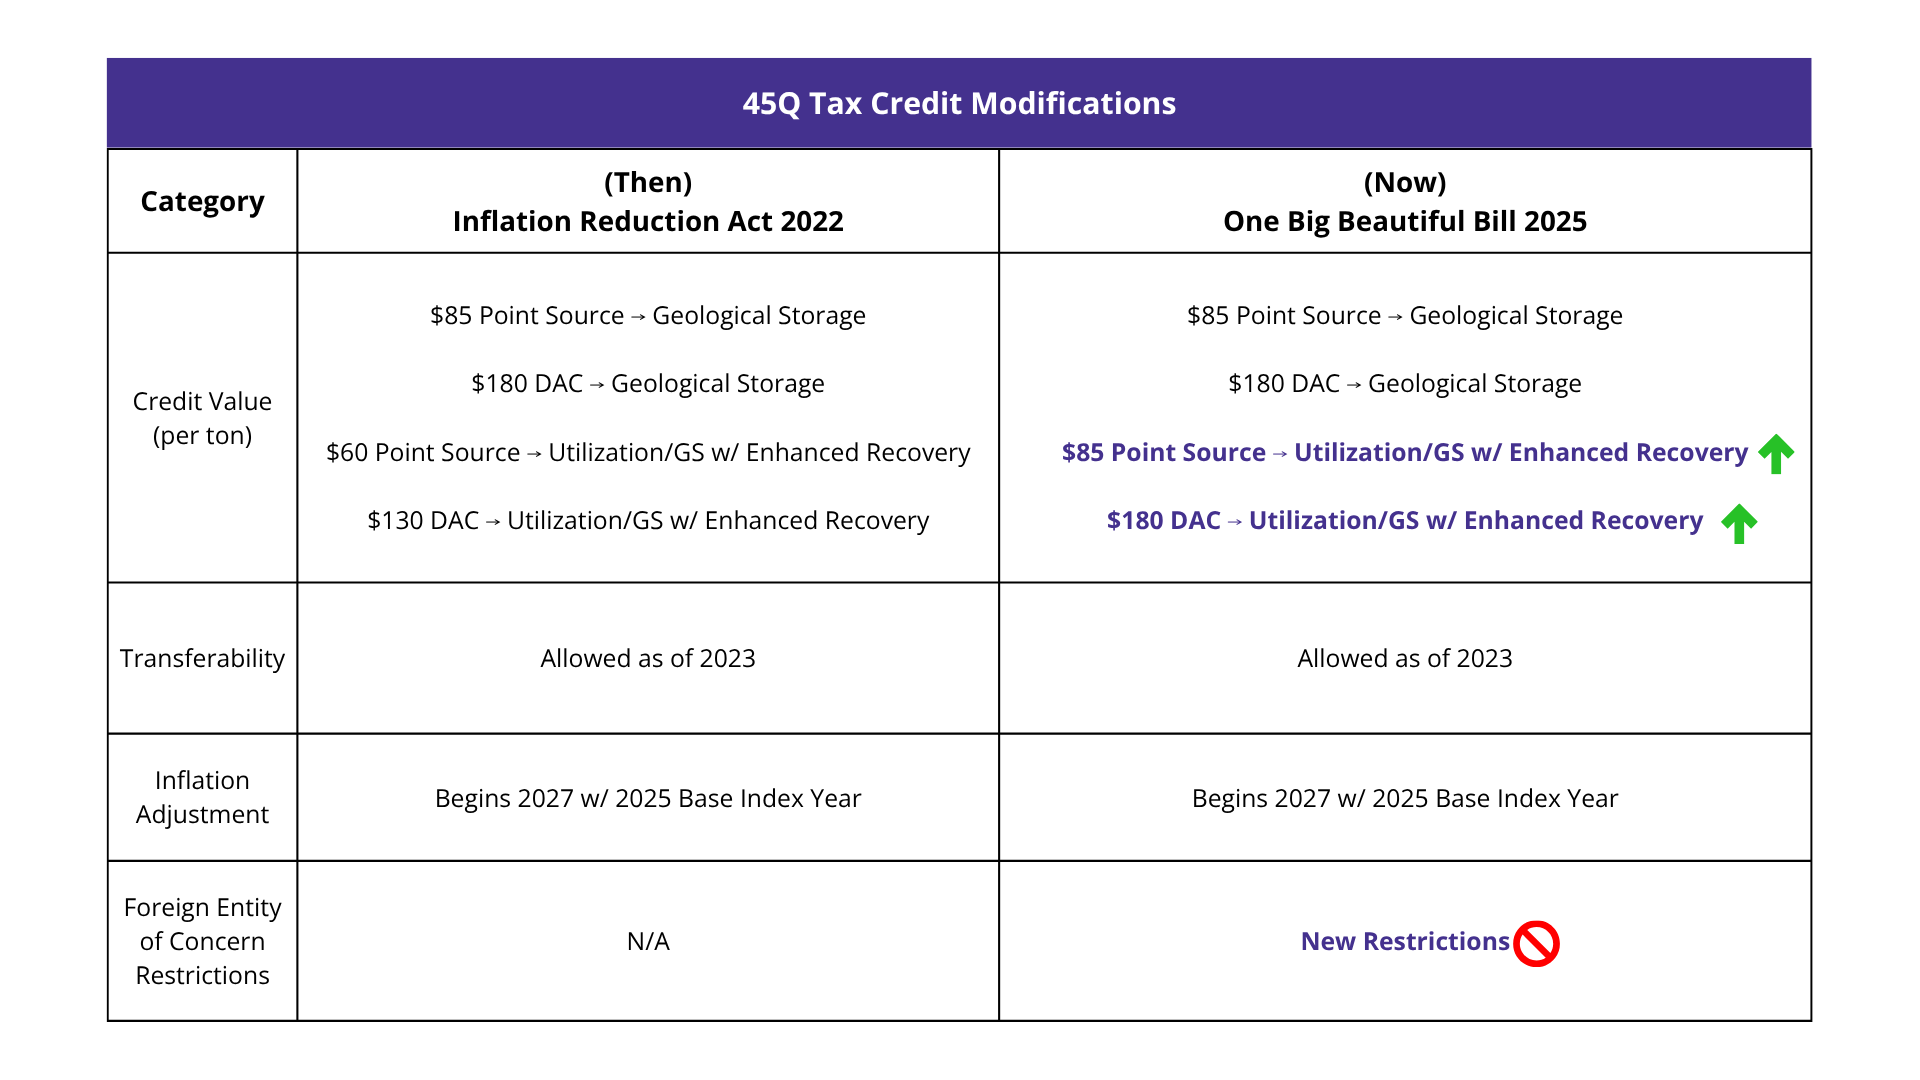
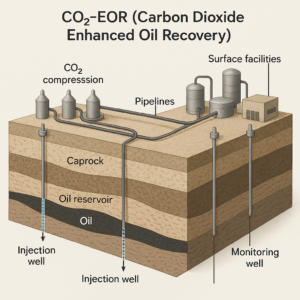
The recently passed One Big Beautiful Bill Actpreserved and enhanced carbon capture and storage (CCS) opportunities. One of the most impactful provisions for carbon capture is the expansion of the 45Q tax credit to $85 per metric ton for CO₂ used in Enhanced Oil Recovery (EOR) when the CO₂ is permanently stored in geological formations.
This update significantly improves the financial outlook for oil and gas developers pursuing CO₂-EOR projects that meet geological sequestration criteria. In this article, we break down the implications of this policy shift and how project developers can capitalize on it.
What’s New in 45Q Under the One Big Beautiful Bill?
The One Big Beautiful Bill Act preserves and enhances the 45Q tax credit structure, with a critical clarification:CO₂ used in EOR now qualifies for the full $85/ton credit if it is geologically sequestered.This aligns EOR with saline storage projects in terms of credit value, provided the CO₂ is not vented or recycled but permanently stored underground in accordance withthe EPA Class VI well regulations.
Key Provisions:
$85/ton for CO₂ captured and geologically stored, including via EOR
$60/ton remains for CO₂ used in EOR without geological storage
Transferability and direct pay options remain intact
No sunset clause, offering long-term certainty for developers
This change reflects growing recognition of EOR’s role in both emissions reduction and domestic energy production.
Three 45Q Benefits for CO2-EOR Project Developers
1. Higher Credit Value = Better IRR
The jump from $60 to $85/ton for qualifying EOR projects can significantly improve project economics. For example, a facility capturing 500,000 tons of CO₂ annually, means an additional $12.5 million/year in direct payments.
2. Geological Storage Is Now a Strategic Differentiator
Projects that integrate Class VI-compliant injection wells and robust monitoring, reporting, and verification (MRV) protocols can now access the higher credit tier. This incentivizes developers to design for permanence and compliance from day one.
Modular Deployment Reduces Risk and Cost in 45Q-Qualified Projects
CO2 projectsrequirements still incentivize modular execution. Incorporating modular process packages and construction not only reduces risk related tofield construction, it’s a strategic tool for moving scope that is governed by 45Q labor requirements onsite to offsite scope; providing lower costs overall and less liability due to prevailing wage.
Why Modular Execution Matters:
Reducing Risk for 45Q Wage Requirements
Offsite labor is not subject to prevailing wage reporting or apprenticeship metrics, allowing the project to source market rate labor offsite and lowering the burden cost for the project.
Only onsite labor requires detailed reporting for compliance tests for 45Q. Shifting scope to offsite locations reduced the cost of compliance.
Cost Control
Onsite scope is exposed to risks from weather delays and increased mobilization costs to site. These costs can be better controlled in a fabrication facility, reducing contingency estimates for the project.
Labor demands in regions are affected by activity from all operators and the limited local skill pool. Leveraging offsite fabrication allows for the scheduling of resources will limit risk to shortages.
Timeline Optimization for 45Q Eligibility
Developers can begin construction on initial modules to meet IRS “begin construction” rules under Safe Harbor, securing eligibility while continuing to develop the rest of the project.
Technical Requirements for Qualifying CO₂-EOR Projects
According to the DOE’s CCUS Appendix H, projects must meet several technical criteria to qualify for the $85/ton credit:
High-purity CO₂ supply (typically >95%)
Compression systems capable of delivering CO₂ at 1,200–2,200 psi
Reservoirs with sufficient porosity and caprock integrity
EPA Class VI injection wells for geological storage
MRV plans approved by the EPA or equivalent state authority
Developing a low-cost injection project requires selection of the proper dehydration approach for water-saturated CO2. CANUSA EPC has released dehydration studies for CO2 projects, helping you select the correct technology for your CO2 project.
Strategic Recommendations for CO2 EOR Evaluations
Determine Key Performance Metrics: Execute a FEED study to determine the proper metrics for financial investment; levelized cost per mton of CO2 product, carbon intensity to capture and process the CO2, and utility requirements.
Leverage Modular EPC Execution: Acceleratelead times, improve cost control, and reduce compliance costs with modularized systems.
Engage Tax Equity Partners Early: The $85/ton credit makes your project more bankable — capitalize on it.
Audit Your CO₂ Source: Ensure your CO₂ stream meets purity and volume thresholds to qualify.
Conclusion
The One Big Beautiful Bill Act has solidified the opportunity landscape for CO₂-EOR projects. By extending the $85/ton 45Q credit to EOR with geological storage, it rewards projects that combine carbon mitigation with energy production. For developers ready to meet the technical and regulatory requirements, the path to profitability just got a lot clearer.
Ready to design a CO₂-EOR project that qualifies for $85/ton? Connect with usto explore FEED support, modular compression systems, and turnkey EPC execution tailored for carbon capture and EOR.
The CO2 market is developing rapidly based on regulations, annual governmental commitments, and voluntary carbon markets. Start to understand the CO2 market from an industrial perspective and understand concepts of Co2 sources, capture technology, and marketing of CO2.
Sources: Point Sources, Flue Gas, Production Gas, Atmosphere
CO2 Emissions Trends
CO2 Capture Types – detailed explanation & notes on improvements
How to Market CO2 – EOR, Sequestration, Liquefaction, Pipelines