Industry: Emissions Reduction

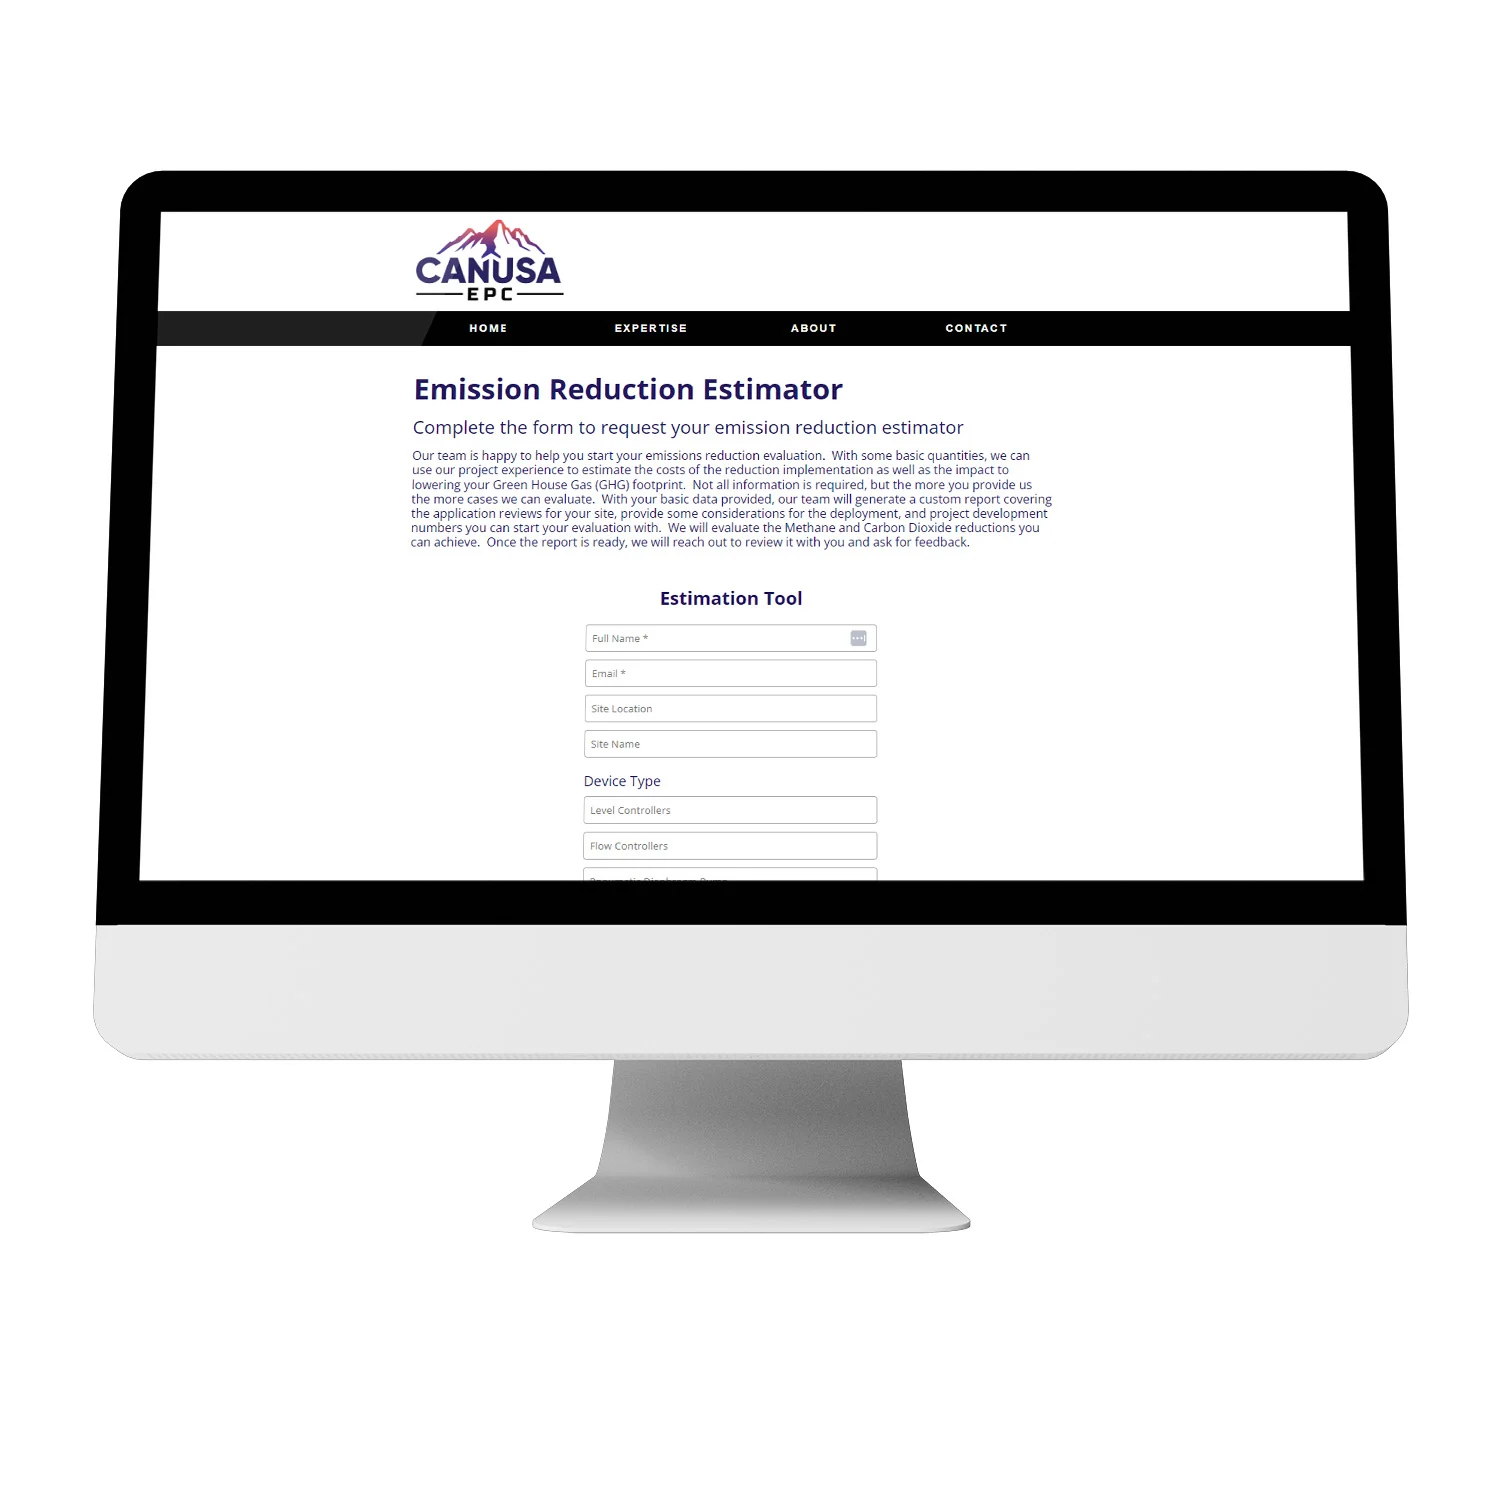
  • Emission Reduction Estimator Tool

    Emission Reduction Estimator Tool

    Summary

    Develop a basis for the evaluation of your emissions reduction efforts in your sites. With some basic quantities, we can use our project experience to estimate the costs of the reduction implementation as well as the impact of lowering your Green House Gas (GHG) footprint.

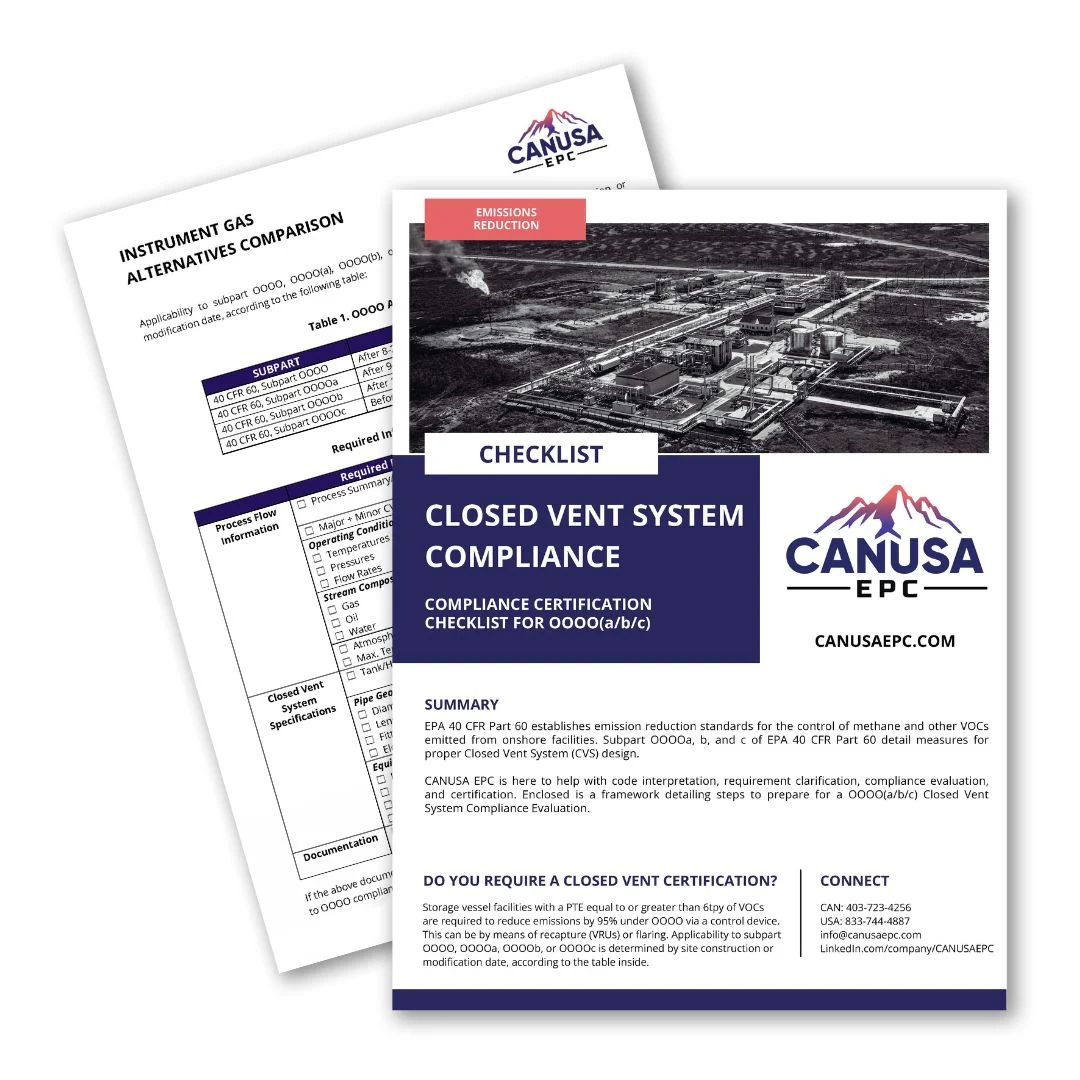
  • Closed Vent System Compliance Certification Checklist For OOOO(a/b/c)

    Closed Vent System Compliance Certification Checklist For OOOO(a/b/c)

    Summary

    EPA 40 CFR Part 60 establishes emission reduction standards for the control of methane and other VOCs emitted from onshore facilities. Subpart OOOO(a/b/c) of EPA 40 CFR Part 60 detail measures for proper Closed Vent System (CVS) design.

    CANUSA EPC is here to help with code interpretation, requirement clarification, compliance evaluation, and certification. Enclosed is a framework detailing steps to prepare for a OOOO(a/b/c) Closed Vent System Compliance Evaluation.

    This guide includes:

    • Applicability Dates
    • Process Flow Information
    • Closed Vent System Specifications
    • Documentation
  • Instrument Air, Nitrogen, or Electric? A Side-by-Side Look at Instrumentation Alternatives for Emissions Reduction Compliance

    Instrument Air, Nitrogen, or Electric? A Side-by-Side Look at Instrumentation Alternatives for Emissions Reduction Compliance

    As the Oil & Gas industry adapts to new environmental standards introduced through the EPA regulation OOOOb, operators are looking for low-emission substitutes for traditional instrument gas systems for pneumatic devices. Factors like power availability, extreme climates, retrofit feasibility, and long-term operating costs influence the most economical and technically viable instrument gas alternatives factor into the decision. 

    Although instrument air is a popular choice for pneumatic devices, there are a variety of instrument gas alternatives that are worth considering. These options include using liquid nitrogen tanks to supply gas to pneumatic devices, using electric actuators on valves, using a combustion-based or compressor-based vent capture system, and implementing low-emission alternatives to traditional pneumatic devices. 


    Controlling Instrument Gas Emissions 

    Natural gas-driven pneumatic devices have been the standard across upstream and midstream oil and gas sites for decades. These systems are simple, reliable, and easy to integrate, but they are a significant source of methane and VOC emissions in the oil and gas industry.  

    In the U.S., regulatory frameworks like EPA “OOOOb” (and soon, “OOOOc”) have required the transition away from traditional instrument gas systems. EPA Subpart OOOOb section 60.5390b requires operators to “design and operate each process controller affected facility with zero methane and VOC emissions to the atmosphere”, beginning January 22, 2027. The regulation includes mandatory monitoring and reporting for all facilities.    

    In Canada, producers are adopting emissions reduction strategies to align with both internal and external ESG targets, investor expectations, and net-zero commitments. 

    Controlling instrument gas emissions by implementing low-emission alternatives is the future of the industry.  

    The challenge? Each instrument gas alternative comes with its own trade-offs. Let’s evaluate! 


    Key Considerations 

    These three considerations often stall progress or lead to overbuilt systems that don’t actually meet site needs. These are the top 3 we see: 

    1. Site Limitations 

      Power availability, space constraints, and environmental conditions will determine what is feasible.
    2. Budgeting & ROI 

      Every solution requires both CAPEX & OPEX. Liquid nitrogen systems, while low in initial cost, come with recurring delivery fees. Electric actuators are expensive, power-intensive, and, on existing sites, require retrofitting of every actuated valve.
    3. Technology Trade-offs 

      Each alternative has a unique set of pros and cons. Some offer zero emissions but require significant upfront investment. Others are easier to implement but come with ongoing operational costs or limited scalability. 


    Comparing the Top Alternatives for Traditional Instrument Gas Systems  

    Instrument Air Systems

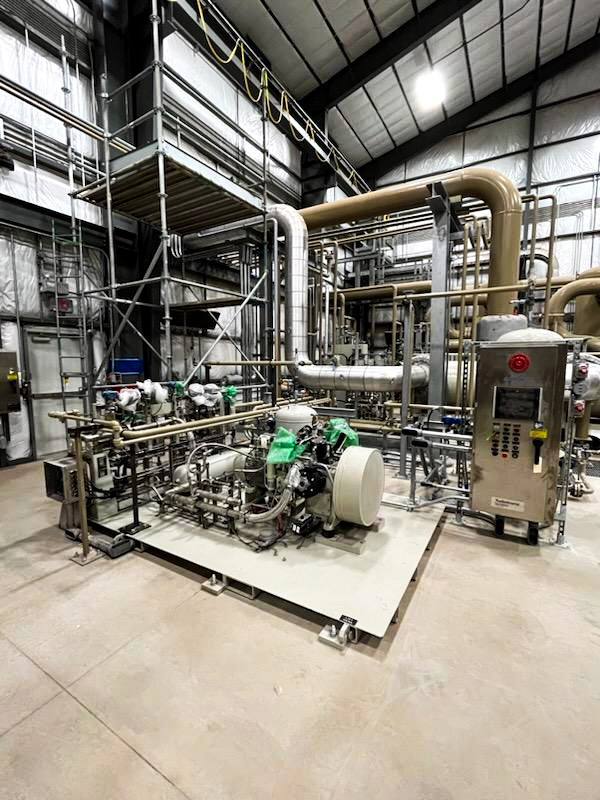
    Instrument air is one of the most established alternatives to gas-driven pneumatics, particularly in midstream facilities. These systems use electric-driven compressors to deliver clean, dry air to valves and controllers, eliminating methane emissions entirely. 

    Pros: 

    • Easy integration  
    • Eliminates all process controller emissions – OOOO(b) compliant with no continued reporting 
    • Compatible with most existing pneumatic devices 
    • Product saved – no longer using sales gas to operate pneumatic devices 
    • Air is non-corrosive and abundant 
    • Expandable to pneumatic pumps and other emission reduction efforts (i.e. start air) 

    Cons: 

    • Introduces an additional piece of rotating equipment  
    • Requires power and space for compressors and dryers  
    • Higher upfront capital costs  
    • Possible rework of existing piping   
    • Introduces an oxidizer into pneumatic lines  
    • Increased operational effort due to required maintenance and troubleshooting  

    Best for: Midstream or central facilities with power availability.

    Vendors Offering Compression: UECompression Packages 

    • 5 HP or 15 HP Reciprocating Packages 
    • Duplex Recip. Package 
    • 5 HP Rotary Scroll  
    • Custom Packages 


    Liquid Nitrogen Supply Systems 

    An option for remote or off-grid sites, liquid nitrogen provides a zero-emission, power-free alternative for driving pneumatic equipment. Suppliers deliver nitrogen in pressurized vessels, and nitrogen is passed through regulators to send vaporized nitrogen to drive pneumatic devices. 

    Pros: 

    • Easy integration 
    • Eliminates all process controller emissions – OOOO(b) compliant with no additional reporting 
    • Product saved – no longer using sales gas to operate pneumatic devices 
    • Pros over air – no additional rotating equipment 
    • Pros over gas – removes requirements for reporting to the EPA 
    • N2 is inert and does not provide an oxidizer into the process 
    • No additional power requirements 
    • Easily scalable & reliable  
    • No upfront capex requirements 
    • Minimal operator involvement 
    • Minimal seasonal, weather, or temperature implications 

    Cons: 

    • Requires regular nitrogen delivery (every 30–60 days) – adds to OPEX, delivery scheduling, risk of delays/impact to schedule 
    • Safety concerns with the addition of a pressurized vessel 
    • Not yet widely used, may face internal approval challenges 

    Best for: Small well pads or facilities without power infrastructure.

    Vendors Offering Liquid Nitrogen Systems: Kathairos Solutions  

    • Provides services through the full timeline for integration, from site assessment to commissioning, monitoring, reporting, and operation. 


    Electric Valve Actuators 

    Electric actuators provide an emissions-free solution to control valve actuation, eliminating the need for access to pneumatic supply lines. They’re ideal for on/off valves in remote pipeline applications. 

    Pros: 

    • Emission-free 
    • Self-calibrating 
    • Low energy requirement 
    • Can be used in low temperature operation 
    • No need for routing of pneumatic lines 
    • Remote monitoring and configuration are available 
    • Solar-powered options are available – remote, power-free pipeline applications 

    Cons: 

    • Significant upfront capex – not realistic for large facilities with many actuated valves  
    • Slow response time – not suitable for tight process control  
    • Not suitable or realistic for existing facilities – requires significant modification to existing valves  
    • May not eliminate the need for pneumatic systems; other pneumatic signal users may exist apart from control valves  
    • Limited applicability as an emissions reduction technology in industry   
    • New technology – lack of familiarity or approval with clients and operators  
    • Although additional energy requirement and cable routing.   
    • Cannot operate on loss of power  

     Best for: Remote oil and gas sites with few pneumatic valves, and no additional pneumatic users. 

    Vendors Offering Electric Actuation: Emerson  

    • Varied applications suited for shut-down valves and control valves.  
    • Offering range of sizes and duty cycles. 


    Combustion-Based Vent Gas Capture 

    This strategy captures emissions from gas-driven pneumatics and routes them to a combustor, converting natural gas into CO₂. Although this method requires continued reporting with the EPA, it can offer OOOOb compliance with minimal disruption in operations.

    Pros: 

    • Can continue to use instrument gas, no need to modify existing piping  
    • Eliminates need for additional rotating equipment, leading to equipment and operational savings  
    • Low initial Capex (if combustor is existing on site)  
    • No additional power requirements  
    • Possible tank battery applications – routing captured pneumatic emissions to tank venting header  

    Cons: 

    • Requires design and installation of a cover that can capture emissions from existing equipment 
    • Only realistic if there is an existing combustor that captured emissions can be routed to 
    • Significant engineering and design time 
    • Does not fully eliminate emissions from pneumatic devices. Monitoring and reporting are still required for OOOO(b) compliance 

    Best for: Facilities with an existing combustor and limited resources for a full system overhaul.


    Capturing Compressor Emissions for Instrument Gas Use 

    This approach captures small amounts of vented gas from compressors and reuses it to power pneumatic devices. It’s a creative way to minimize waste and emissions using existing infrastructure. 

    Pros: 

    • Reduces total emissions from compressors 
    • Removes the need for header routing to compressors 
    • No additional power requirements 
    • Marginal increase in sales of gas 
    • OOOO(b) compliance for compressor emissions capture and process controllers 

    Cons: 

    • Significant engineering and design time, modification of on-skid piping 
    • Does not fully eliminate emissions from pneumatic devices. Monitoring and reporting are still required for OOOO(b) compliance. 

    Best for: Sites looking to improve compressor efficiency or reduce emissions without installing new systems. 


    Which Pneumatic Emissions Reduction Technology is Best?  

    There are numerous technologies available to reduce or eliminate emissions from instrument gas lines, whether it be implementing solutions within an existing instrument gas system, adopting instrument air or vaporized nitrogen, or utilizing electrically actuated valves. Although instrument air has been the most widely used pneumatic signal alternative within the industry, operators should understand that other technologies exist and may be a more practical solution for eliminating instrument gas emissions.  

    The technologies available allow for flexibility in a wide range of applications. There are options for sites with limited power availability, existing facilities looking to retrofit or upgrade their traditional instrument gas system, remote pipeline operations, and new facilities looking to build out with an emissions-free pneumatic system.   

    At CANUSA EPC, we help operators make informed decisions based on real-world experience. We’ve seen the nuances of site power, valve density, weather risk, and regulatory targets. 

    When you’re ready to talk instrumentation upgrades or emissions strategies, we’d be happy to share what’s working in the field.  

    __________ 

    FURTHER EMISSIONS-REDUCTION READING  

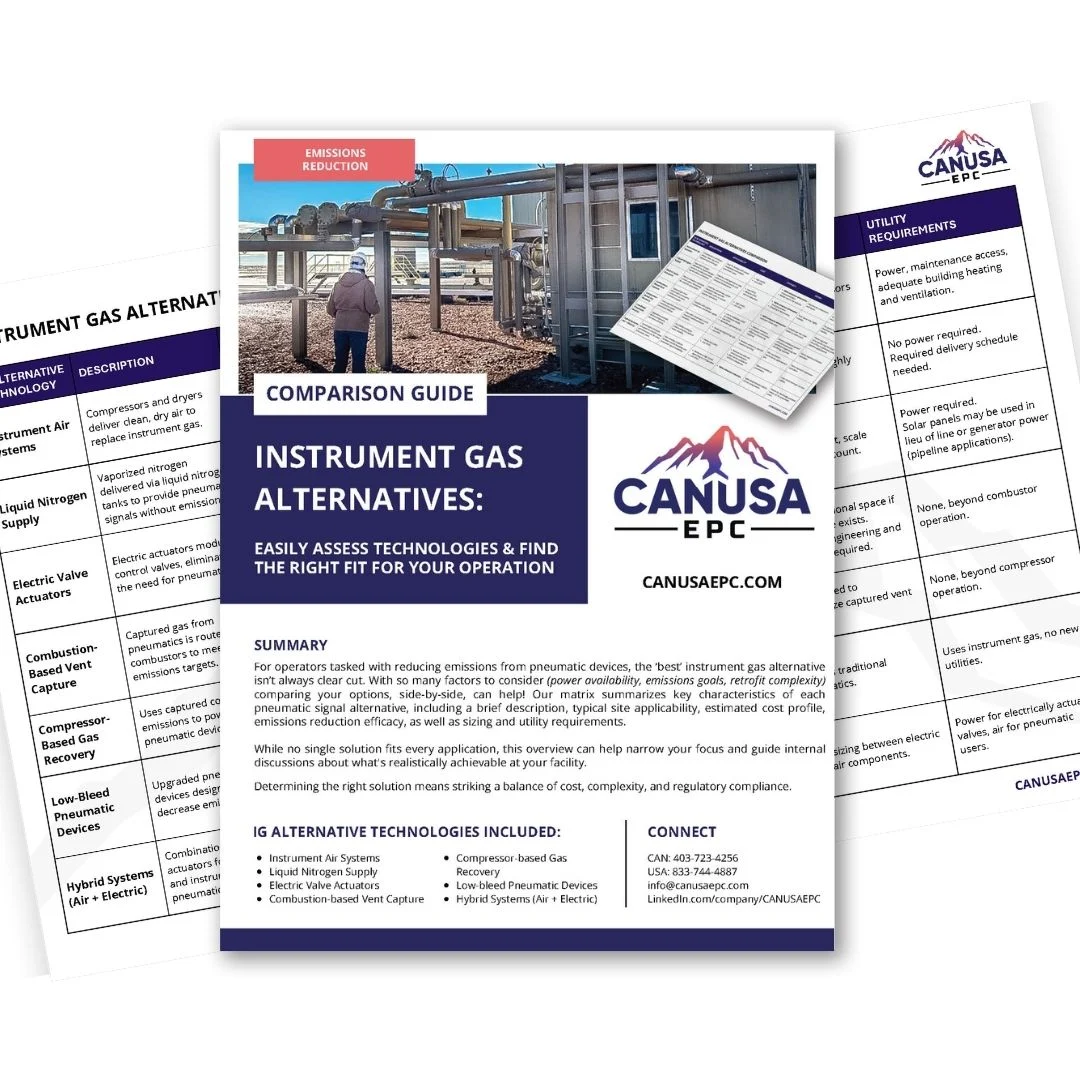
    Instrument Gas Alternatives Comparison Guide
    To accompany this blog, we have created a free comparison guide for your convenience. Download the Instrument Gas Alternatives Comparison Guide.

    OOOO(b) for Compression Sites: Cost-Management Strategies for Methane Reduction
    Want to ensure you meet budget and timelines? Read on for 7 strategies to consider.
    __________ 

    Author(s) 

    Megan Hurley, Engineer I 

    External Sources 

    1. https://www.epa.gov/natural-gas-star-program/rulemakings-policy-and-laws-address-methane-emissions-oil-and-gas-sector#:~:text=Methane%20Emissions%20Standards,-Final%20Rules%20to&text=In%202024%2C%20EPA%20issued%20a,methane%20emissions%20from%20existing%20sources.&text=In%202016%20%2D%20EPA%20issued%20three,permitting%20requirements%20for%20the%20industry. 
    2. eCFR :: 40 CFR Part 60 Subpart OOOOb — Standards of Performance for Crude Oil and Natural Gas Facilities for Which Construction, Modification or Reconstruction Commenced After December 6, 2022  
    3. https://www.canada.ca/en/services/environment/weather/climatechange/climate-plan/2035-emissions-reduction-target.html 
  • OOOO(b): Methane Emission Reduction Cost-management Strategies for Compression Sites

    OOOO(b): Methane Emission Reduction Cost-management Strategies for Compression Sites

    Summary

    The EPA’s latest methane rule – OOOO(b) – mandates zero-emission process controllers and pneumatic pumps, pushing gas compression facilities to invest in compliance projects. Want to ensure you meet budget and timelines? Read on for 7 strategies to consider in your compliance project program.

    This whitepaper compiles data from previous projects and studies to support the financial analysis for power generation projects for operators determining what is the best onsite power solution for their project.

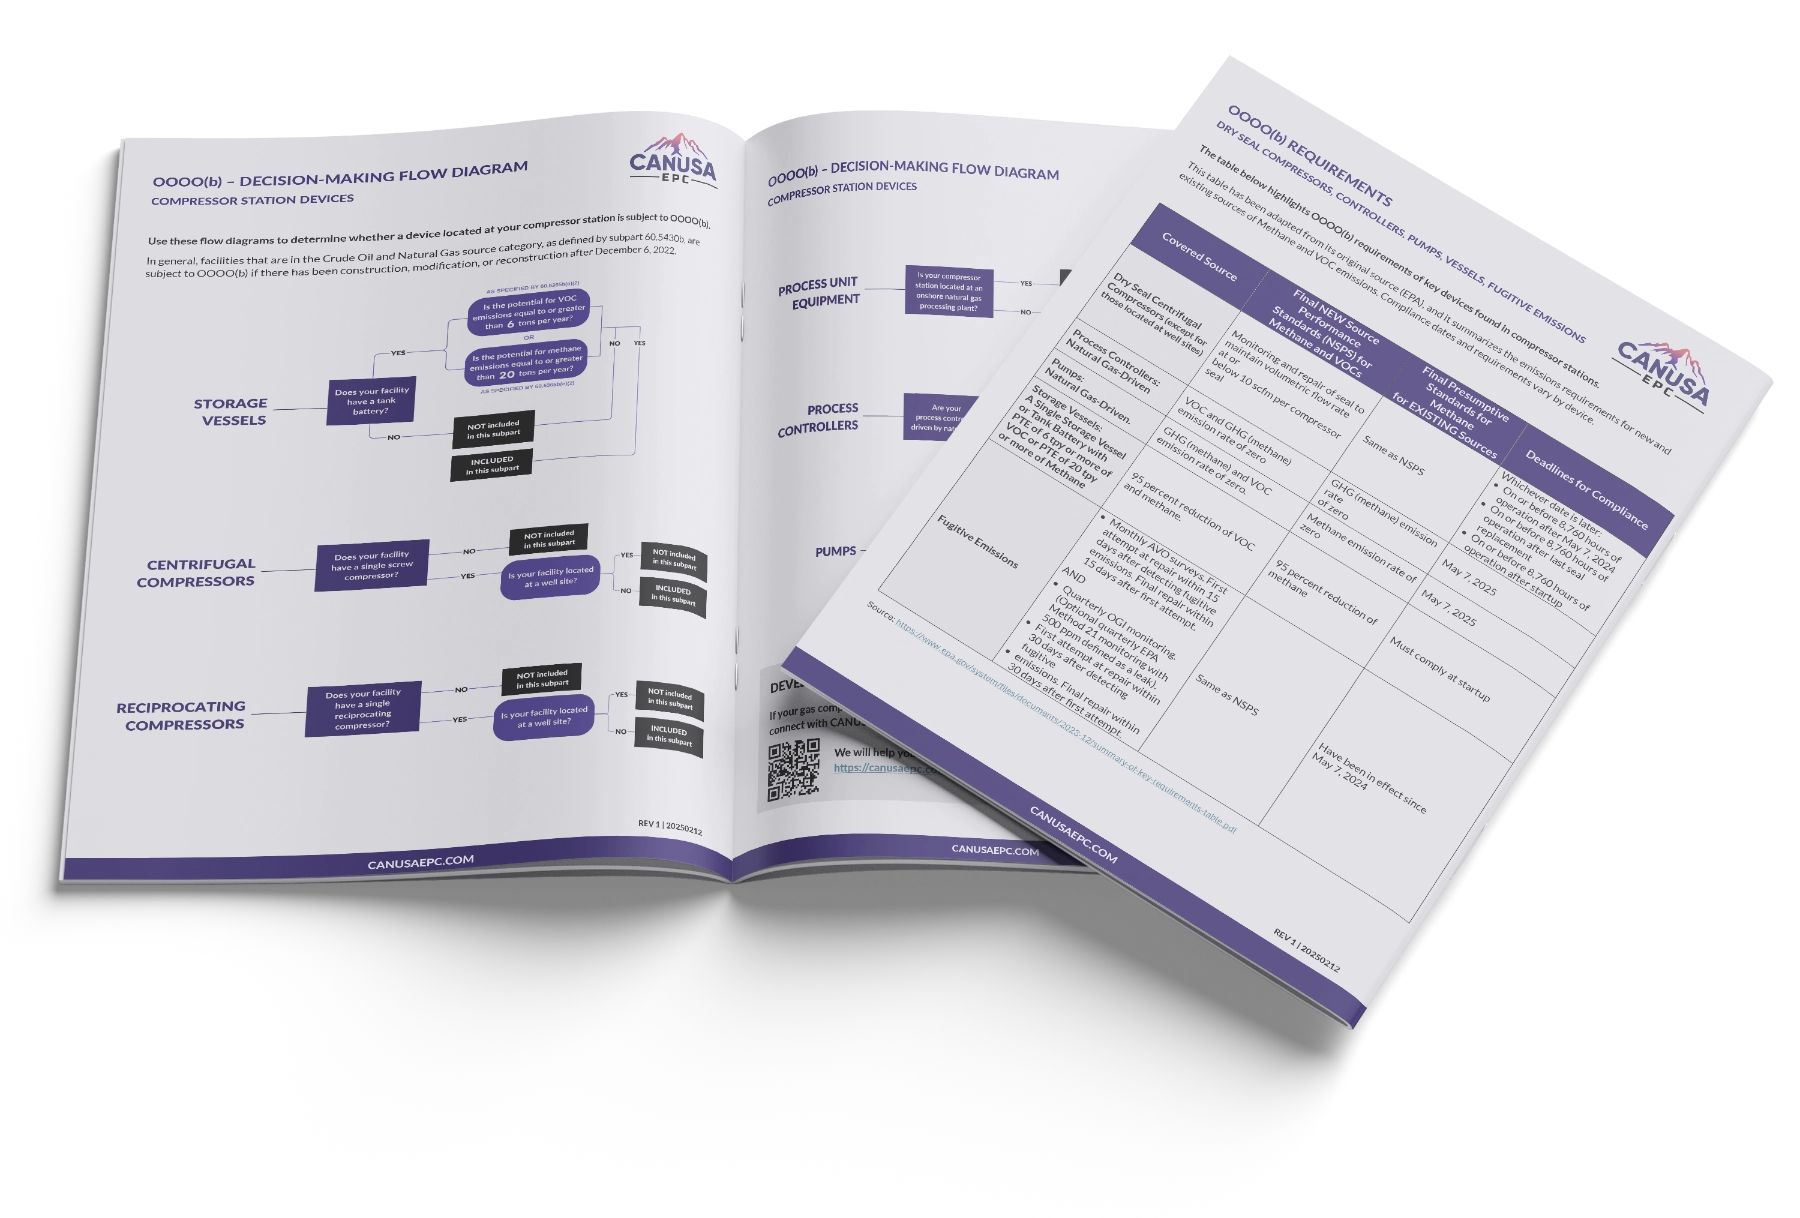
    This OOOO(b) for compression sites guide includes:

    • Article, published in Hart Energy Magazine, discussing instrument air conversions, OOOO(b) planning and best practices, achieving operational efficiencies, and moving forward with compliance
    • Matrix highlighting OOOO(b) requirements of key devices found in compressor stations: dry seal compressors, controllers, pumps, vessels, and fugitive emissions
    • Decision-making flow diagrams to help you determine which OOOO(b) sub-parts pertain to your operation
  • Instrument Gas Alternatives Comparison Guide

    Instrument Gas Alternatives Comparison Guide

    Summary

    For operators tasked with reducing emissions from pneumatic devices, the ‘best’ instrument gas alternative isn’t always clear cut. With so many factors to consider (power availability, emissions goals, retrofit complexity) comparing your options, side by-side, can help! Our matrix summarizes key characteristics of each pneumatic signal alternative.

    While no single solution fits every application, this overview can help narrow your focus and guide internal discussions about what’s realistically achievable at your facility. Determining the right solution means striking a balance of cost, complexity, and regulatory compliance.

    This instrument gas alternatives comparison guide includes:

    • Brief Description
    • Typical Site Applicability
    • Estimated Cost Profile
    • Emissions Reduction Efficacy
    • Sizing and Utility Requirements
  • Instrument Gas to Instrument Air Conversion

    Instrument Gas to Instrument Air Conversion

    The Challenge

    The Client needed to convert the instrument gas devices at (4) natural gas compression facilities in Oklahoma to instrument air service in a 6-month period.

    OOOO(b) requires that process controllers emit no identifiable emissions. Instrument air systems are inherently emissions free, so they are not subject to requirements specified in subpart 60.5390b.

    The Solution

    CANUSA EPC conducted site visits to audit all the instrument gas users at the facility, as-build the P&IDs for IA users, and validate facility electrical capacity to add an instrument air skid. Sizing requirements for the instrument air compressor skid were provided to account for all users and start air for the natural gas compressors.

    The design and construction packages were executed in sequential order to meet accelerated schedule deadlines.

    Engineering

    • Walk down (4) facilities
    • Instrument demand study
      • Start air evaluation
    • Instrument air skid specifications
      • Dual compressor design for
    • Recommend electrical upgrades

    Design

    • Isometric riser details for IA user areas
    • Header design to account for future start air
    • Electrical and utility upgrades

    The Results

    Reduction in fugitive emissions and venting from previous IG users and compression start-up

    • Successfully achieved reduction of all instrument gas users
    • Calculated emissions reduction of 153 MTPY of methane
    • Compliance with OOOO(b) section 60.5390b
    • 25% reduction in engineering design on a site basis
  • Tank Venting Emissions Reduction

    Tank Venting Emissions Reduction

    The Challenge

    The Client was venting excessive vapors from their produced water tank battery due to higher operating pressure in their inlet separator. Operations had determined that the pressure drop between the slug catcher and the storage tank was resulting in entrained gas venting above OOOO(b) limits.

    The Solution

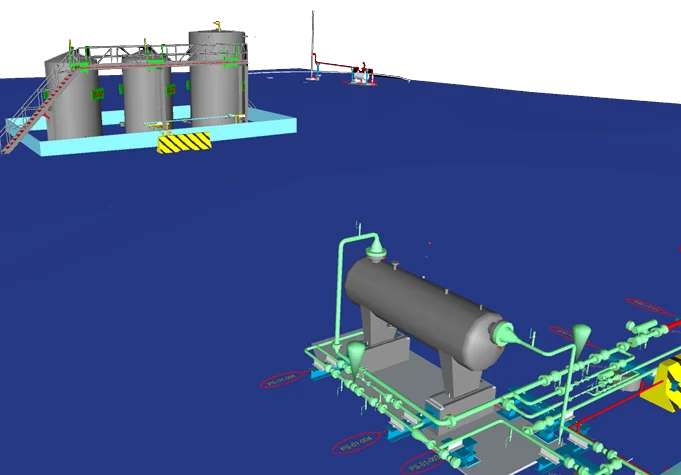
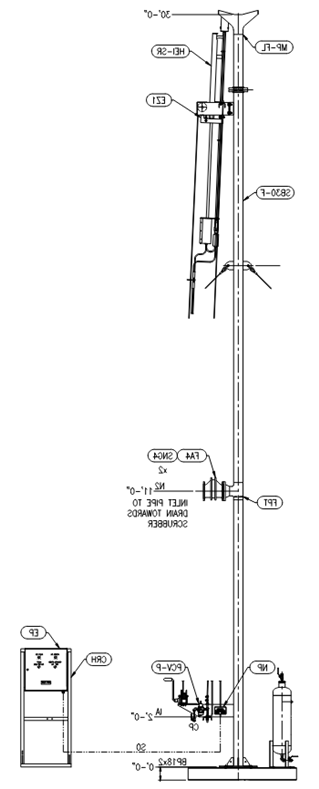
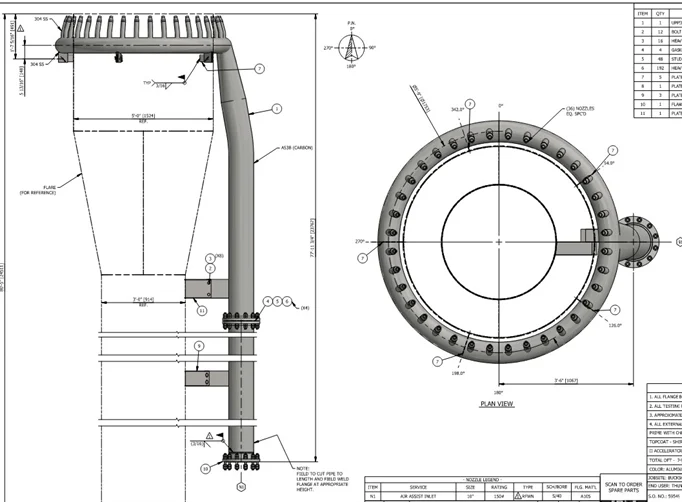
    CANUSA EPC provided engineering and design to install an emission control device. An intermediate knockout drum and combustor were added to the facility. Liquids were routed from the slug catcher to the lower-pressure intermediate knockout, allowing more gases to flash off before sending the remaining liquids to the water tanks. All flashed gases were sent to the combustor.

    Engineering

    • Flare specification
    • Re-purposed knockout drum evaluation
    • Instrumentation and control systems added
    • Saddle design and flare guy wire anchoring solution

    Design

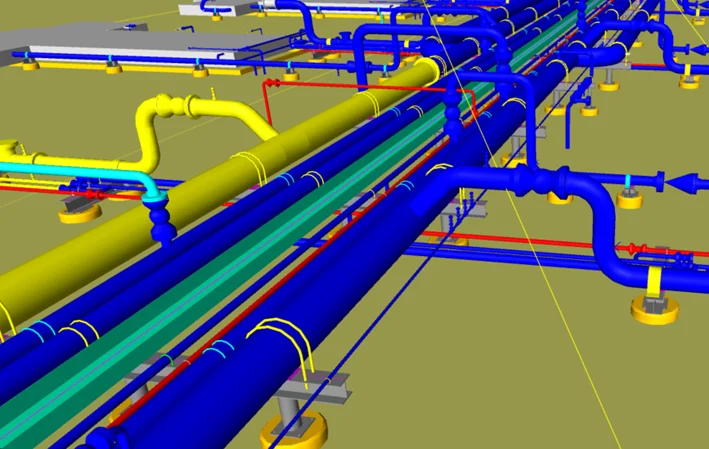
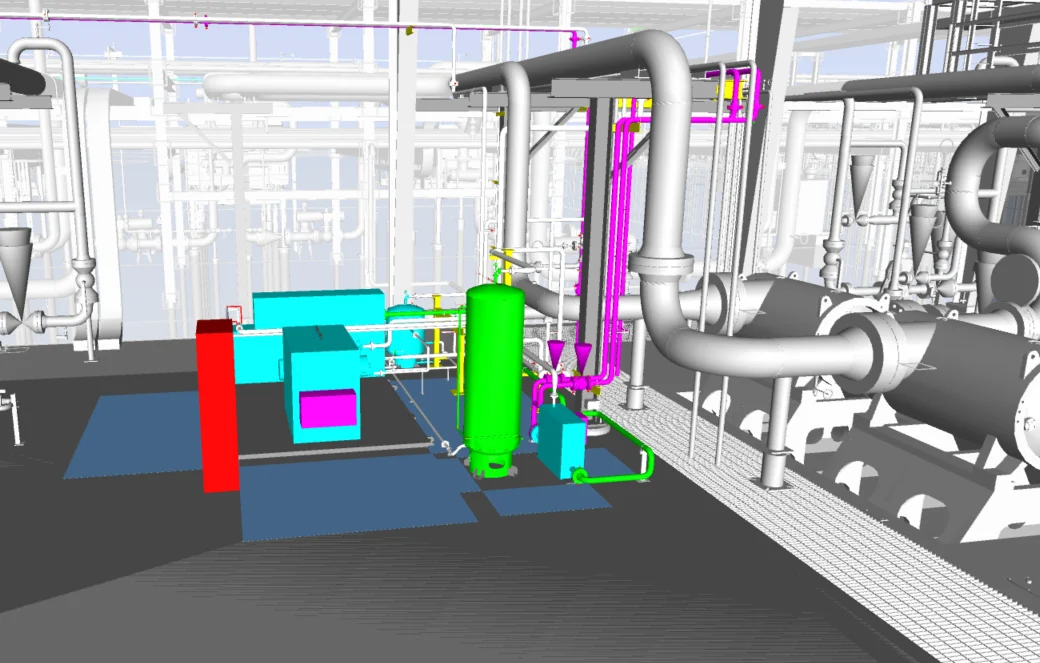
    • 3D Modeling of piping, structural steel, and foundations
    • Piping isometrics
    • Pipe support and foundation details

    The Results

    Reduction in vented vapors from the tank battery

    • Reduced direct venting methane by 10 TPY
    • Alternative solution for recycle of entrained gas to inlet
    • Compliance with OOOOb section 60.5365b(e)
  • Amine Vent Dispersion

    Amine Vent Dispersion

    The Challenge

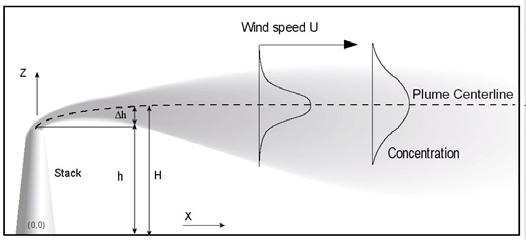
    The Client was experiencing shutdown trips in their amine processing area from hydrogen sulfide sensors due to increased H2S in the inlet gas. During calm ambient conditions (e.g. no wind), the gas from the vent stack can migrate to grade and present safety concerns for the onsite operators and exceed the NIOSH REL and OSHA PEL 10-minute exposure limits.

    The Solution

    CANUSA EPC evaluated various options from thermal oxidizers, vent stack blowers, and H2S scavengers as solutions to reduce the instances where H2S was causing facility shutdowns. The solution selected was a modified blower vent tip system to increase the velocity of the exit gas to elevate the concentrated gas high enough to disperse to non-detectable levels by the time it reached safety sensors.

    Engineering:

    • Blower specification
    • Dispersion modeling
    • Electrical system additions
    • Vent structural steel design for blower

    Procurement:

    • VFD Specification
    • Blower package evaluation
    • Dispersion modeling
    • Construction package bids

    The Results

    Reduction in ground measurements of H2S exceeding the 20 ppm sensor shutdown

    • Reduced conditions where operators are exposed to H2S limits above OSHA
    • Mitigated instances of shutdown related to inadequate dispersion of H2S
  • Turbine Seal Gas Capture

    Turbine Seal Gas Capture

    The Challenge

    The Client agreed to mitigate emissions from turbine units seal gas system at one of their compression sites to satisfy an EPA consent decree regarding the Clean Air Act and the Colorado Air Pollution Prevention and Control Act. Per the terms of the agreement, the Client was required to install a seal gas capture system within 90 days of receiving the dry seal recompression unit.

    The Solution

    CANUSA EPC worked with the Client and packager of the dry seal recompression system to develop an engineering and design package for the installation of the system.

    Multi-Discipline Engineering

    • Electrical tie-in of 40 HP Motor
    • PSV sizing for new relief scenarios
    • Piping modeling for discharge into plant inlet to recover the gas
    • Automation design to integrate with station controls

    Procurement

    • VFD and Cable specification
    • Pressure Instrumentation
    • Construction Bid Walkdowns

    The Results

    Deployed the first seal gas system in the fleet

    • Installation of a single capture unit for seal gas of two turbine units

    Reduction in fugitive methane emissions

    • Reduction in venting emissions of 49.3 mton of CO2e/day
  • Reduced Emissions with Heat Recovery

    Reduced Emissions with Heat Recovery

    The Challenge

    CANUSA EPC was tasked with adding heat trace (piping freeze protection) and building heat to a gas plant. It was noted that there was a large amount of waste heat being released into the atmosphere from cooling oil at the adjacent oil battery. The Client wanted to investigate if there were options to utilize this waste heat, reducing operating costs and GHG emissions. The heat source was provided at 60°C where typical glycol heating systems operate at a minimum of 90°C.

    The Solution

    The heat duty required for providing heat to the facility was approx. 3.5MMBTU/hr and the heat duty available from cooling the oil was 10MMBTU/hr. CANUSA EPC designed a unique system based on a proprietary calculation model to utilize the warm glycol exiting the oil cooler at 60°C.

    Developing a Plan to Meet Client Expectations

    • Leveraged our in-house process and design experts
    • Developed and managed installation scope to meet existing project schedule

    Sourced New Equipment:

    • Glycol boiler
    • Glycol cooler
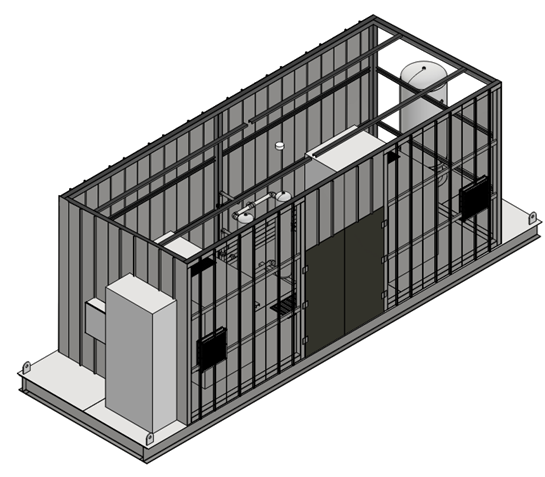
    • Waste heat recovery building
    • Glycol pump
    • Glycol heat trace and supply/return manifolds
    • Glycol building heaters

    Execute Value Engineering to Support the Project Schedule

    • Rigorous heat duty and heat transfer calculations to maximize efficiency
    • Hydraulic modeling of the GHT system
    • GHT and manifold isometrics to control costs of installation

    The Results

    Lowered emissions of the facilities

    • Eliminated 4.4 MTPD of CO2 equivalent emissions

    Lowered annual facility operating costs

    • Estimated $100,000+ CDN/year OpEx savings

    Integrated waste heat recovery

    • Designed and implemented a GHT system to operate with 60⁰C warm glycol